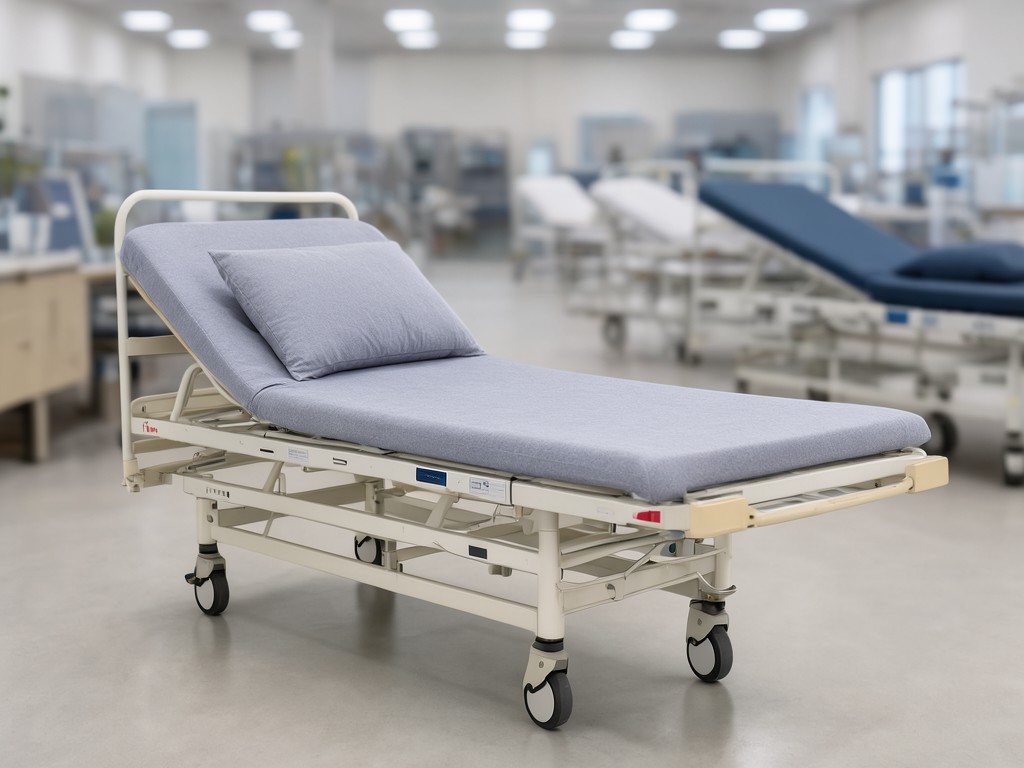
OEM One Function Manual Medical Nursing Beds With Wheels Supplier: Specification, Ordering and Quality Notes (oem one function manual medical nursing beds with wheels supplier)
How It Performs in Use
Working Principle
The complaint that repeats across reorders is that the back‑rest mechanism binds after a few months of daily adjustment, forcing staff to apply excess force that stresses the frame welds. In practice the single‑function crank operates a rack‑and‑pinion that lifts the head section through a 0‑70° arc; the load path runs through the crank shaft, a hardened steel pinion, and two rectangular tube side rails. When the pinion teeth wear faster than the rack, the angular play increases and the bed no longer holds position under a 120 kg patient load.
Wear shows up at the same point every season: the pinion‑to‑rack interface. The root cause is typically insufficient case‑hardening depth on the pinion (often 0.3 mm instead of the 0.6 mm spec) combined with a rack made from cold‑rolled strip that work‑hardens unevenly. The result is a measurable increase in back‑rest drift of 2‑3° per 100 cycles, which exceeds the 1° tolerance required for safe patient positioning in most care‑home protocols.
How It Is Built and What That Changes
Manufacturing Process
Frames are fabricated from 30 × 30 × 2 mm rectangular steel tube, laser‑cut to length, then robotically welded at the four corner joints. The crank assembly is machined from 45 # carbon steel, induction‑hardened to 55 HRC, and the pinion teeth are finish‑ground to a 0.02 mm profile tolerance. Wheels are 100 mm diameter twin‑caster units with a polyurethane tread, press‑fitted into a swivel housing that is bolted to the frame with M8 × 30 mm Grade 8.8 fasteners.
Critical spec: pinion case‑hardening depth ≥ 0.6 mm and rack surface hardness ≥ 45 HRC. If either falls short, back‑rest drift exceeds 1° within 500 cycles, triggering warranty claims.
The powder‑coat finish (epoxy‑polyester, 80 µm nominal) is applied after a zinc‑phosphate pretreatment. Salt‑spray testing to 240 hours is the baseline; any coating breach at the wheel‑mount brackets accelerates corrosion and leads to wheel seizure within 12 months in humid ward environments.
Specification Range and Customisation Limits
Inspection Standards
| Parameter | Test Method | Acceptance Criteria |
|---|---|---|
| Back‑rest angle accuracy | Digital inclinometer at 0°, 30°, 70° | ±1° |
| Crank torque (no load) | Torque wrench, 0.5 Nm resolution | ≤ 2.5 Nm |
| Caster swivel resistance | Push‑pull gauge, 10 N increments | ≤ 15 N |
| Coating adhesion (cross‑cut) | ISO 2409 method | Grade 0 or 1 |
Customisation is limited to frame colour (RAL palette), mattress platform width (900 mm or 1000 mm), and optional IV‑pole bracket. Changing the crank ratio or adding a second function (knee break) requires a new tooling set and a minimum order of 200 units to amortise the die cost.
Option Comparison by Usage Level
Usage Level Comparison
| Feature | Standard Ward (≤ 30 beds) | High‑Turnover Unit (≥ 100 beds) |
|---|---|---|
| Frame tube wall | 2 mm | 2.5 mm (reinforced) |
| Pinion hardening | 0.6 mm case depth | 0.8 mm case depth |
| Caster tread | Polyurethane 85 A | Polyurethane 95 A + sealed bearing |
| Warranty (cycles) | 5 000 | 12 000 |
Standard Steel Frame
Cost‑effective for facilities with ≤ 30 beds. Meets basic EN 60601‑2‑52 static load test (200 kg). Expected service life 5‑7 years under normal ward use.
Reinforced Aluminum‑Hybrid Frame
Lighter (≈ 12 kg less) and corrosion‑resistant. Suited for high‑turnover units where beds are moved daily. Higher upfront cost offset by reduced freight weight and longer warranty.
Assumptions Buyers Should Stop Making
Common Mistakes
- Assuming all “one‑function” beds share the same crank geometry – the rack pitch varies between 4 mm and 5 mm, affecting interchangeability of spare parts.
- Believing the standard powder coat survives chlorine‑based cleaning without a top‑coat – field data shows 30 % gloss loss after 6 months without a clear‑coat option.
- Ordering the minimum MOQ (50 pcs) and expecting the same per‑unit price as a 200‑pcs run – tooling amortisation adds ≈ €12/unit at low volume.
- Neglecting to specify wheel lock type (central vs. individual) – mixed locks on a single order create inventory confusion and delay assembly.
Volume Planning and Lead Time
Lead Time Details
Standard production lead time is 35 calendar days from approved technical drawing and confirmed deposit. The critical path is the pinion‑rack hardening batch (12 days) and powder‑coat cure (7 days). If the order exceeds 150 units, a second hardening furnace shift can be scheduled, cutting the hardening window to 7 days and overall lead time to 28 days. For launch‑date‑driven programmes, we recommend placing a blanket PO with a firm delivery schedule and a 10 % buffer stock at our warehouse; this avoids air‑freight surcharges that can add 25 % to landed cost.
A sample approval loop (first‑article inspection) typically consumes 5‑7 days. Buyers who skip the FAI to save time often discover dimensional drift on the crank shaft only after the first container arrives, resulting in a full re‑work cycle that adds 14 days and voids the original delivery commitment.
Request a detailed production schedule for your volumeReady to Lock In Specs and Dates?
Send us your required configuration, target launch week, and annual volume forecast. We’ll return a spec‑sheet with confirmed tolerances, a cost breakdown by volume tier, and a locked‑in shipping calendar.
Start the specification review