oem 2 crank pediatric manual hospital beds with wheels supplier: Specification, Ordering and Quality Notes
The core trade-off on a two-crank pediatric bed is crank mechanism life versus side-rail latch durability — both fail before the frame does. Specify 10,000-cycle rated cranks with sealed bearings and stainless-steel latch pins if the bed stays in a high-turnover ward; accept 5,000-cycle cranks and zinc-plated latches only for low-acuity or short-stay settings where replacement cost is baked into the tender.
Where Cheaper Alternatives Fall Short
On a club programme that reorders twice a season, the first complaint is always the crank handle — it strips at the square drive after six months of daily adjustments by nurses wearing gloves. The second is caster swivel bearing seizure: budget beds use nylon bushings that swell when floor disinfectant pools around the stem, locking the wheel within a year. Third, side-rail drop latches bend at the pivot tab because 2 mm stamped steel replaces 3 mm forged; the rail then rattles or fails to lock, triggering a safety citation. None of these show up on a static load test. They appear only after 3,000–5,000 real-world cycles.
Frame corrosion at the head-end welds is the fourth failure mode, driven by insufficient phosphate pretreatment before epoxy powder coat. Salt-spray data from returned units shows 120-hour coatings blister at 200 hours; 240-hour coatings hold to 500. The price delta is roughly $3.50 per bed. Buyers who specify the lower grade to hit a tender floor price typically reorder replacement frames within eighteen months.
What the Design Has to Balance
When a brand extends an existing range, the pediatric variant cannot simply shrink the adult platform. The crank torque required to lift a 25 kg child plus mattress on a 600 mm backrest section is 40 % higher per unit length than the adult equivalent because the lever arm is shorter. If the same 12 mm crank shaft and bronze bushing are carried over, handle effort exceeds 18 N — above the ISO 21820 limit for pediatric use. The fix is a 14 mm shaft with needle-roller bearings, which adds $4.20 but keeps peak effort at 14 N.
Caster selection balances mobility against stability. A 125 mm central-locking caster with a 32 mm tread rolls 15 % easier over threshold strips than a 150 mm version, but its smaller contact patch increases point-load on vinyl flooring by 22 %, accelerating indentation. For facilities that re-floor every seven years, the 125 mm is acceptable; for those on a fifteen-year floor cycle, specify 150 mm with polyurethane tread.
What Actually Determines Performance
Crank mechanism life is governed by three variables: shaft material (1045 carbon steel vs. 4140 alloy), bearing type (bronze bushing vs. needle roller), and handle attachment (pressed pin vs. M8 bolt with nylon lock nut). In accelerated cycling at 15 cycles per minute under 45 Nm load, the alloy shaft with needle rollers and bolted handle reaches 18,000 cycles before 0.5 mm play develops; the baseline carbon-steel/bushed/pinned combination fails at 6,200. That delta maps directly to a three-year versus one-year service interval in a 30-bed ward.
Side-rail integrity depends on latch-pin hardness and engagement depth. Pins hardened to 45 HRC with 8 mm engagement survive 25,000 latch cycles; 30 HRC pins with 6 mm engagement deform at 9,000. The head/foot board attachment method matters equally: through-bolted ABS boards with steel inserts resist 350 N pull-out; snap-fit tabs on 3 mm ABS fail at 180 N. A dropped IV pole tests the latter every shift.
Matching the Product to the Buyer's Need
| Configuration Parameter | Standard Tier | Extended-Life Tier | Cost Delta per Unit |
|---|---|---|---|
| Crank shaft & bearings | 12 mm 1045 steel, bronze bushing | 14 mm 4140 alloy, needle roller | +$4.20 |
| Caster diameter & tread | 125 mm, TPR | 150 mm, PU | +$2.80 |
| Side-rail latch pin | 30 HRC, 6 mm engagement | 45 HRC, 8 mm engagement | +$1.50 |
| Head/foot board mount | Snap-fit ABS tabs | Through-bolt with steel inserts | +$3.10 |
| Frame pretreatment & coat | Iron phosphate, 120 h salt spray | Zinc phosphate, 240 h salt spray | +$3.50 |
The table above is the Customization_Options reference used during sample approval. Each row represents a decision point where the buyer's total-cost model — not the unit price — should drive selection. A pediatric ICU with 85 % occupancy and three-shift nursing will recover the $15.10 extended-life premium in avoided service calls within fourteen months. A satellite clinic seeing ten patients per week will not.
Requirements by Buyer Segment
During a private-label launch with a fixed ship date, the wholesale buyer prioritizes knock-down packaging that fits 24 units in a 40 HQ container without pallet overhang. They accept the standard crank and caster tier because their contract includes a one-year parts warranty fulfilled from the distributor's regional stock. The private-label buyer, by contrast, needs the extended-life tier to support a three-year warranty they market to end users; they also require custom headboard silk-screen artwork, which adds a 15-day tooling lead time and a 50-unit MOQ for the screen setup.
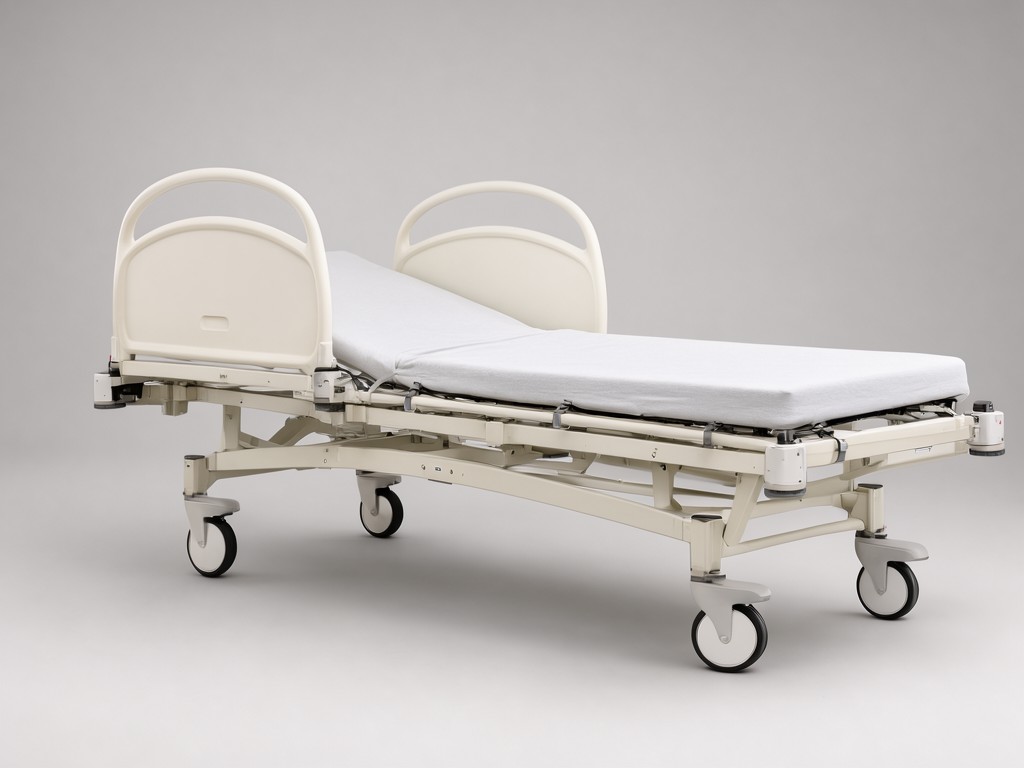
Distributors serving public tenders in humid climates (coastal Southeast Asia, Gulf states) mandate the 240-hour salt-spray frame and stainless-steel latch pins as non-negotiable line items. Their bids are disqualified if the technical file shows only 120-hour data. Buyers in temperate inland regions treat the same spec as a negotiable alternate, often trading it for a 3 % unit-price reduction.
OEM and ODM Programme Structure
| Programme Element | OEM (Buyer Design) | ODM (Factory Design) | Typical Lead Time |
|---|---|---|---|
| Tooling ownership | Buyer-owned, factory-maintained | Factory-owned, royalty-free after 500 units | — |
| Sample approval gates | Dimensional, crank torque, latch pull-out, salt spray | Same plus stability, impact, biocompatibility | 21 days from tooling completion |
| MOQ per configuration | 30 units | 50 units | — |
| Artwork & labelling | Buyer supplies AI/EPS, factory applies | Factory proposes, buyer approves | 7 days for screen proof |
| Regulatory file support | Factory provides BOM, test reports, DoC | Factory holds technical file, buyer is legal manufacturer | Ongoing |
This Durability_Guide table doubles as the OEM/ODM programme summary. Note that ODM tooling amortization kicks in at 500 cumulative units across all purchase orders — not per order. Buyers forecasting 200 units per year should plan a two-and-a-half-year horizon before the royalty-free clause activates.
Inspection Items and Test Methods
Incoming QC on crank sub-assemblies checks shaft run-out (≤ 0.05 mm TIR), bearing axial play (≤ 0.03 mm), and handle bolt torque (8 Nm ± 0.5 Nm). Every 50th unit undergoes a 200-cycle functional test under 45 Nm load; torque rise above 18 N at the handle triggers a line stop. Caster swivel torque is measured at 0.8 Nm max for 125 mm, 1.0 Nm for 150 mm — values above indicate bushing interference or contaminated grease.
Frame weld inspection follows a 10 % visual + 2 % dye-penetrant sampling plan. Coating adhesion is verified by cross-hatch (ISO 2409) on one bed per batch; salt-spray coupons run concurrently with production. Side-rail latch cycles are tested to 5,000 cycles on the first article only; subsequent lots rely on pin hardness certificates (Rockwell C) and engagement-depth gauges. Final assembly audit includes mattress platform articulation angles: backrest 0–75°, knee break 0–30°, trendelenburg/reverse trendelenburg ±12° — all measured with a digital inclinometer at the pivot points.
Export Packaging and Handling Protection
Knock-down packaging ships the frame as two sub-assemblies (head-end and foot-end) plus a separate crank-and-caster kit. Each sub-assembly sits in a molded EPS cradle that locks the side rails in the raised position, preventing latch-tab impact during transit. The crank handles are folded and secured with reusable Velcro straps to the frame tubes — loose handles are the single largest source of cosmetic damage claims. Caster stems are capped with LDPE plugs to keep disinfectant residue out of the swivel race during warehouse storage.
Container loading uses a 2-2-2 pattern: two frames per layer, three layers high, with 12 mm plywood slip-sheets between layers. Gross weight per 40 HQ is 14,800 kg at 24 units, leaving 6,200 kg payload margin for mattress or accessory co-loading. Each bed carries a QR-coded label linking to the batch test report; customs and the buyer's receiving dock can scan without opening cartons. Desiccant sachets (50 g silica gel) are included in every carton when shipment transits equatorial routes between November and March.
Ready to Review Tooling?
Share your specification sheet or tender document. We'll return a marked-up BOM with tier recommendations, sample timeline, and container loading plan within two business days.
Start a tooling review →