Direct Factory steel manual hospital bed for patients Wholesale - Bulk Supply and Specification Guide
Design Constraints Behind the Specification
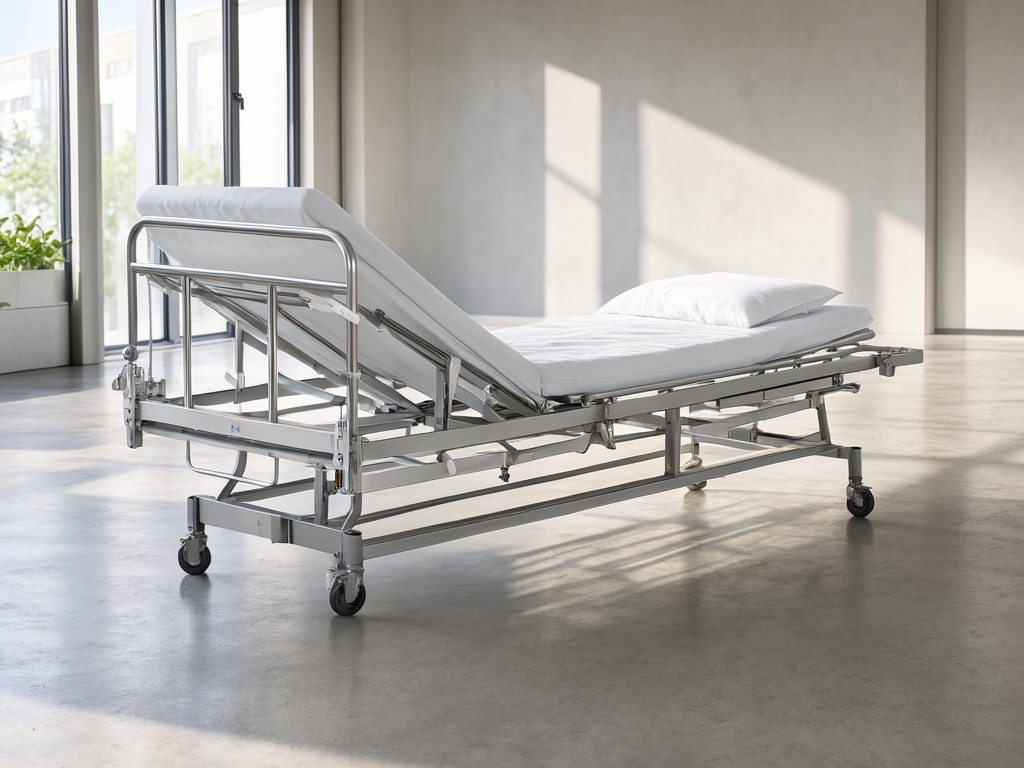
The frame geometry is dictated by the need to support a 250 kg static load while keeping the overall width under 1 000 mm for standard corridor clearance.
- Wall thickness 1.5 mm minimum to meet load rating
- Crank torque limited to 12 Nm for nurse operation
- Caster lock engagement force ≤ 15 N
- Powder‑coat thickness 80‑100 µm for corrosion resistance
- Mattress deck deflection < 5 mm under full load
Size, Weight and Specification Range
Buying Mistakes That Lead to Returns
A common error is selecting the light‑duty crank assembly for a ward that runs 24‑hour cycles.
When the crank rating is undersized, the handle strips after 3 000‑4 000 cycles, forcing the buyer to replace the entire drive train. The failure also shifts the bed’s centre of gravity, causing caster lock drift and increasing the risk of patient transfer incidents. Specifying the heavy‑duty crank (rated 12 Nm, 10 000‑cycle life) eliminates the early‑wear mode and aligns the service interval with the facility’s preventive‑maintenance schedule.
Segment-Specific Requirements
General Ward
- Standard 250 kg load rating sufficient
- Manual crank with 14 turns
- Two braked casters, two swivel
- Powder‑coat, 80 µm minimum
High‑Acuity / ICU
- Reinforced frame, 300 kg rating
- Heavy‑duty crank, 12 Nm, 10 000‑cycle life
- Four braked casters, central lock
- Epoxy‑primer + powder coat, 100 µm
Quality Control and Batch Consistency
Consistency Rule
Frame wall‑thickness tolerance of ±0.2 mm is the single spec that drives load‑rating repeatability across lots.
Each production batch undergoes a 100 % dimensional check on the first article, followed by a statistical sample of 30 frames for wall‑thickness, crank torque, and caster lock force. Salt‑spray exposure (96 h) validates coating adhesion before shipment. Deviations beyond the stated tolerances trigger a hold and root‑cause review, preventing drift that would otherwise surface as warranty claims after installation.
Capacity, Tooling and Scheduling
Lead time is driven by four sequential constraints that cannot be overlapped without additional tooling investment.
- Raw‑steel coil allocation – 2 weeks for certified grade
- Stamping die changeover – 3 days per profile set
- Powder‑coat line scheduling – 1 week for colour batch
- Final assembly and functional test – 2 days per 200‑unit lot
Packing, Marking and Freight Configuration
| Parameter | Flat‑pack (knock‑down) | Pre‑assembled |
|---|---|---|
| Carton dimensions (L×W×H) | 2 200 × 1 050 × 250 mm | 2 200 × 1 050 × 750 mm |
| Gross weight per unit | 55 kg | 62 kg |
| Units per 40‑ft HC | 84 | 56 |
| Handling time at destination | 30 min (assembly) | 5 min (position only) |
| Damage risk (transit) | Low (components protected) | Medium (exposed frame) |
Ready to lock in artwork and branding for your private‑label run? Submit your logo files and we’ll return a pre‑production proof within 48 hours.
Request artwork review