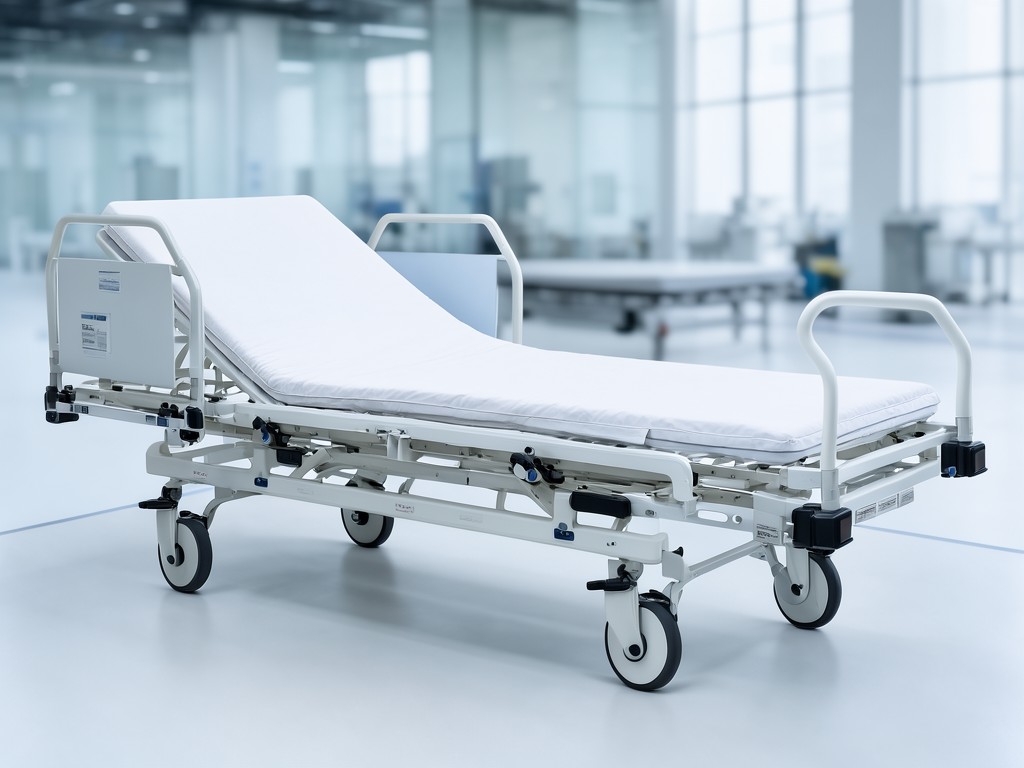
Direct Factory single function manual hospital beds with mattress Company - Bulk Supply and Specification Guide
The build method decides the cost structure: cold‑rolled steel frames are stamped, welded, then powder‑coated in a single line, while the mattress core is moulded from high‑density polyurethane foam and wrapped in a welded‑seam PVC cover. First‑article tooling determines the dimensional envelope for every subsequent unit, so any change to frame gauge or foam density after the initial run requires a new die set and a full re‑qualification cycle.
Process choice shows up later as warranty claims: a 1.5 mm frame with standard epoxy coating typically yields a 250 kg static load rating and 8 000 articulation cycles before coating wear appears, whereas a 2.0 mm frame with zinc‑rich primer plus epoxy topcoat pushes the rating to 300 kg and extends coating life beyond 12 000 cycles. The mattress IFD (indentation force deflection) is set during foam pour; a 120 N IFD provides a firm surface for acute care, while a 90 N IFD reduces pressure‑point risk for long‑term patients.
Material Options and Their Trade-offs
Frame gauge and coating choice drive cost and service life.
Grade A – 1.5 mm cold‑rolled steel, epoxy powder coat
Static load 250 kg, coating wear visible after ~8 000 cycles, unit weight ~38 kg.
Best for budget‑driven tenders where replacement cycle is 3–4 years.
Grade B – 2.0 mm cold‑rolled steel, zinc‑rich primer + epoxy topcoat
Static load 300 kg, coating intact beyond 12 000 cycles, unit weight ~44 kg.
Preferred for high‑turnover wards and contracts demanding 5‑year service intervals.
Measured Performance in Real Use
Load rating and cycle life are the primary acceptance criteria.
Each production lot is subjected to a static load test at 1.25 × the rated capacity for 5 minutes, followed by a cyclic articulation test at 0.5 Hz for the specified cycle count. Mattress IFD is measured on a 200 mm diameter indenter at 25 % compression. Coating adhesion is verified by cross‑hatch tape pull after salt‑spray exposure. Results are logged per batch and traceable to the first‑article report.
| Test | Standard Reference | Acceptance Criteria | Frequency |
|---|---|---|---|
| Static load | Internal spec (derived from IEC 60601‑2‑52) | No permanent deformation at 1.25 × rated load | Every lot |
| Articulation cycles | Internal endurance protocol | ≥ 8 000 cycles (Grade A) / ≥ 12 000 cycles (Grade B) without functional loss | Every lot |
| Mattress IFD | ASTM D3574 (adapted) | 120 N ± 10 % (acute) / 90 N ± 10 % (long‑term) | Every lot |
| Coating adhesion | ISO 2409 (cross‑hatch) | Rating 0 or 1 after 96 h salt spray | First article + quarterly audit |
How to Choose Before Requesting a Quote
Define the clinical environment before requesting a quote.
- Specify maximum patient weight and required safety factor.
- Select mattress firmness (IFD) based on care level.
- Confirm side‑rail configuration: fixed, fold‑down, or removable.
- State cleaning protocol (chemical agents, frequency) to match coating chemistry.
- Indicate any integrated accessories (IV pole, drainage bag hook).
Customisation Options and Their Limits
Colour, side‑rail style, and mattress cover fabric are the most common variables.
Custom colours require a minimum order of 200 units and add 15 days to the lead time because the powder‑coat line must be flushed and re‑validated. Mattress cover fabric changes (e.g., anti‑microbial vinyl vs. standard PVC) trigger a new foam‑cover bonding qualification.
Branding artwork is applied by silk‑screen on the headboard panel; the print area is 300 mm × 150 mm, resolution 300 dpi, and colours are matched to Pantone solid coated swatches. Logo placement tolerances are ±2 mm.
Segment-Specific Requirements
Acute‑care wards demand faster height adjustment and integrated IV poles.
Long‑term care facilities prioritise lower mattress IFD, removable side rails for transfer ease, and a coating system that withstands daily quaternary‑ammonium disinfection. Home‑care units often request a reduced overall width (≤ 900 mm) to fit standard doorways, which forces a narrower frame profile and a lighter mattress core (≈ 30 kg). Each segment drives a distinct combination of frame gauge, coating, and mattress specification that must be locked in the first‑article drawing set.
Working as a Production Partner, Not a Catalogue Supplier
First‑article approval locks tolerances before volume production.
Drawing revision control is managed through a shared PLM folder; any dimensional change after sign‑off requires a new first‑article run and a signed deviation waiver from the buyer’s quality engineer.
Sample approval includes a physical inspection of weld bead consistency, coating thickness (measured by magnetic gauge, target 80 µm ± 10 µm), and mattress cover seam integrity. Artwork proofs are printed on the actual headboard substrate for colour verification before the production run commences.
Packing, Marking and Freight Configuration
Flat‑pack frames on pallets reduce freight volume by 30 %.
Each bed ships as two sub‑assemblies: the frame (folded flat) and the mattress (rolled, vacuum‑sealed). Pallets are 1 200 mm × 1 000 mm, stacked 4 high, with corner protectors and stretch‑wrap. Every unit receives a barcode label encoding model, batch, and serial number; the master carton label duplicates this data for warehouse scanning. Export shipments include a fumigation‑free wood declaration and a certificate of conformity referencing the first‑article test report.
Ready to finalize artwork and branding? Contact us to start the first‑article review.