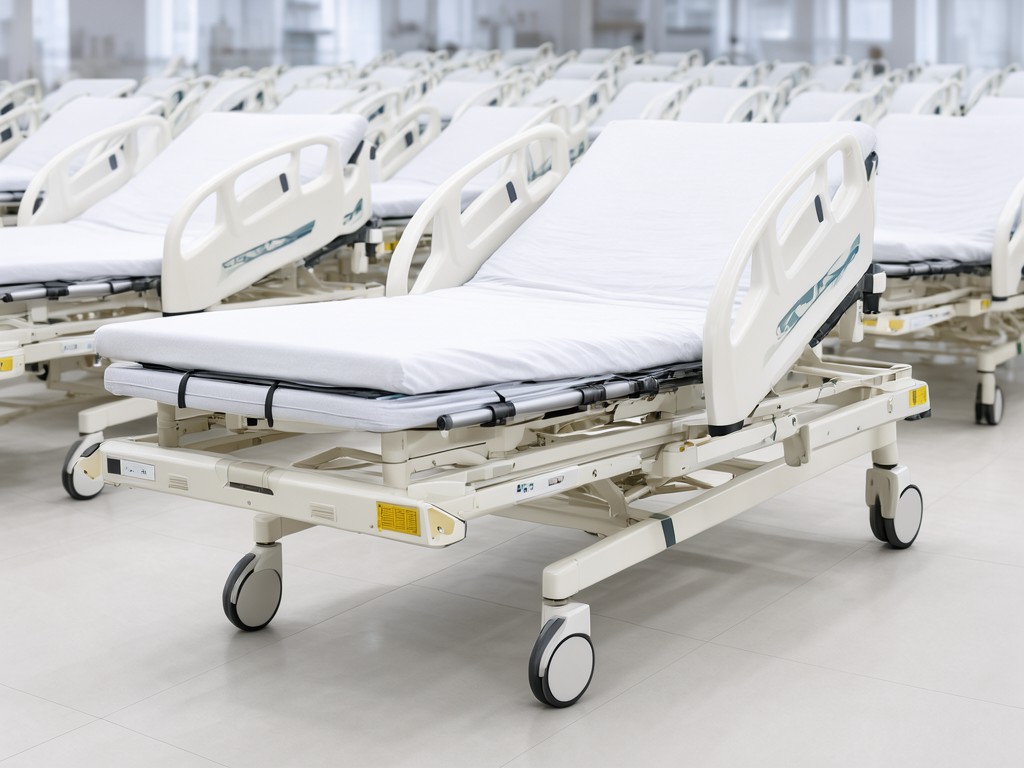
Selection Trade‑off: Crank Torque vs. Wheel Lock Life
Before comparing quotations, two suppliers quoting the same specification can show unit price and service life diverge because the double‑crank gear hardness and caster lock cycle rating are not tied to the CE mark alone. A higher gear hardness (≈ 58 HRC) extends crank life by 30 % but adds €12‑€18 per unit; a caster rated for 100 k lock cycles reduces wheel‑replacement frequency in high‑turnover wards. The buyer must decide which cost driver dominates the total cost of ownership.
Specifying CE Certified double crank hospital bed with wheels manufacturer for Wholesale and OEM Orders
What the Design Has to Balance
In a 30‑bed ward the bed frame sees 12‑15 crank cycles per patient per day; the gear train must transmit 150 Nm without permanent deformation, while the four 125 mm casters must survive 80 k lock/unlock events per year. The powder‑coat thickness (80‑100 µm) protects the 2 mm steel tube from saline cleaning agents, yet excessive thickness adds weight that pushes the shipping volume over the 0.85 m³ per pallet limit. Balancing gear hardness, caster rating, and coating thickness determines whether the unit stays under the 45 kg per bed freight ceiling.
Lot‑to‑lot drift in gear tooth profile (± 0.02 mm) translates into a 5 % variance in crank effort after 10 k cycles, which shows up as nurse‑reported “stiffness” complaints and drives warranty claims. Controlling the heat‑treat window to ± 5 °C keeps the hardness spread within 2 HRC, limiting that drift.
Matching the Product to the Buyer's Need
Private‑label buyers typically specify a back‑rest angle range of 0‑75° and a knee‑break range of 0‑30°, both driven by the same double‑crank shaft. If the OEM requires a 90° back‑rest for bariatric protocols, the crank arm length must increase by 15 mm, which raises the required gear torque to 180 Nm and forces a larger motor housing – a cost jump of roughly €22 per unit. Importers targeting the EU public‑tender market often lock the caster spec to a 100 k cycle rating and a 150 kg static load, because the tender documents reference EN 12531‑2 for mobility. Selecting the 125 mm polyurethane‑tread caster with a sealed bearing meets both without a redesign.
A specification table clarifies the configurable envelope:
| Parameter | Standard Range | Typical Value | Notes |
|---|---|---|---|
| Back‑rest angle | 0‑75° | 70° | 90° optional with longer crank arm |
| Knee‑break angle | 0‑30° | 25° | Fixed per CE file |
| Crank torque rating | 150‑180 Nm | 150 Nm | Higher rating adds €12‑€18 |
| Caster lock cycles | 80 k‑100 k | 100 k | Polyurethane tread, sealed bearing |
| Frame weight (incl. mattress platform) | 42‑46 kg | 44 kg | Keeps pallet under 0.85 m³ |
| Powder‑coat thickness | 80‑100 µm | 90 µm | Salt‑spray 500 h per EN ISO 9227 |
Assumptions Buyers Should Stop Making
A common assumption is that the CE mark guarantees identical crank feel across batches; the mark only confirms that the design meets essential requirements, not that the gear hardness tolerance is held to ± 2 HRC. Another assumption is that any 125 mm caster can be swapped without affecting the bed’s dynamic stability – the offset between caster centre and frame centreline changes the tipping moment by up to 3 Nm, which can push a borderline design over the EN 60601‑2‑52 limit. Finally, buyers often treat the powder‑coat as a purely aesthetic layer; in reality the 90 µm epoxy‑polyester barrier is the primary defence against chloride‑induced pitting in wards that use hypochlorite wipes daily.
What Gets Checked Before Shipment
Each production lot undergoes a dimensional audit (± 1 mm on overall length, width, height), a crank torque test at 150 Nm for 5 000 cycles with torque decay logged, a caster lock‑cycle test to the rated 100 k cycles with bearing temperature monitored, and a coating adhesion cross‑hatch (ISO 2409) after 500 h salt spray. Beds that show > 5 % torque decay or any coating delamination are held for rework. The inspection report is packaged with the shipment and referenced in the certificate of conformity.
Stock Availability and Reorder Planning
Standard configuration (150 Nm crank, 100 k caster, 90 µm coat) is kept in a safety stock of 120 units, replenished on a 6‑week production lead time. Custom crank torque or caster rating adds a 2‑week tooling set‑up and a minimum order quantity of 40 units to amortise the gear‑heat‑treat batch. Buyers planning a 12‑month rollout should place a blanket order with quarterly releases; this locks the gear hardness lot and prevents the ± 0.02 mm tooth‑profile drift that appears when separate heat‑treat lots are mixed.
Request a pre‑production sample or discuss a blanket‑order schedule.
Contact our sales engineering team